Can OLED Suppliers in Different Countries Share Qualification Criteria?
OLED suppliers in different countries can share qualification criteria when those criteria describe the same application, use the same test methods, and require comparable evidence. Buyers can establish a common baseline for optical performance, reliability, electrical behavior, manufacturing controls, and traceability. That baseline makes international sourcing easier to compare and gives engineering teams a consistent basis for approving alternatives.
Approval still needs boundaries. A panel qualified for an indoor handheld terminal may be unsuitable for a continuously illuminated control display, even if both meet the same initial brightness specification. Likewise, technical qualification does not establish compliance in every destination market. The practical approach is to share a core qualification protocol, then attach requirements for the intended product, manufacturing site, and sales region.
Start with the display’s actual duty, not the supplier’s country
Before comparing suppliers, define what the OLED must do throughout the product’s service life. Without that definition, a common checklist can create misleading equivalence: two suppliers may report matching specifications while testing under different conditions or supplying different module configurations.
For smart terminals and AI-IoT equipment, the application profile should describe screen content, operating hours, ambient light, temperature exposure, brightness control, and expected replacement intervals. Persistent dashboards, navigation elements, and status icons deserve particular attention because uneven pixel use can produce differential aging. A display used intermittently for setup has a different exposure profile from one showing the same interface throughout every shift.
Also define the boundary of the item being qualified. A bare panel, a display module with a driver circuit, and a bonded assembly with cover glass and touch sensing are different qualification objects. Optical coatings, adhesives, mechanical support, and thermal conditions can affect the assembled result. Evidence for a panel alone cannot establish the performance of every assembly built around it.
A useful qualification specification connects each requirement to an operating condition and an acceptance decision. Instead of requesting “high brightness,” specify the measurement conditions, required operating modes, and acceptable performance after relevant aging exposure. Instead of requesting “long lifetime,” identify the degradation mechanisms that would make the product unacceptable.
The buyer should settle four questions before issuing a shared protocol:
- Which display behaviors affect usability or the product’s essential functions?
- What environmental and usage conditions must the display tolerate?
- Which characteristics must remain interchangeable across suppliers?
- What evidence will support approval, and what changes will invalidate it?
These decisions keep the comparison focused. Suppliers can propose different technical solutions, but they must demonstrate suitability against the same application requirements.
Make the common criteria measurable and the evidence comparable
The strongest candidates for international standardization are requirements that can be measured independently of manufacturing location. Optical performance, electrical characteristics, interface behavior, defect acceptance, and reliability outcomes belong in this shared core. Manufacturing quality controls and traceability can also follow a common framework, although the evidence must identify the actual production operation.
Optical performance needs a common measurement recipe
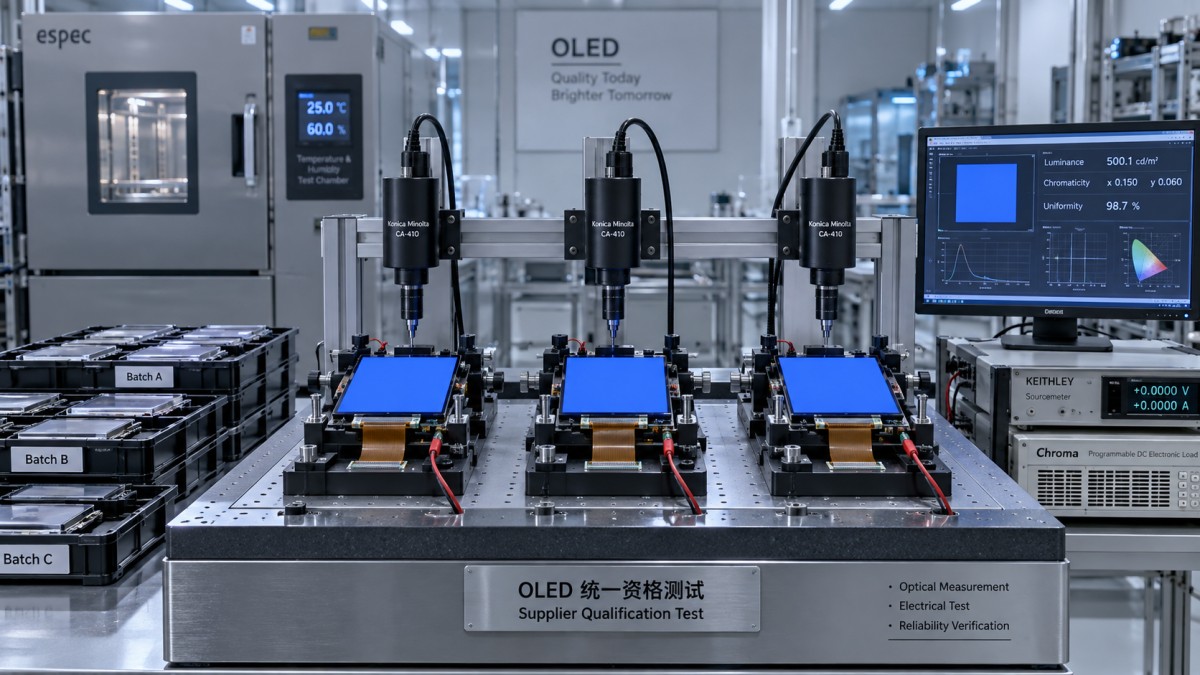
Brightness, color coordinates, uniformity, viewing behavior, and visible defects are useful comparison points only when the measurement setup is controlled. Displayed image content, illuminated area, drive settings, temperature, stabilization time, and measurement geometry can influence results. A supplier’s headline brightness value provides limited guidance if those conditions are missing.
For OLEDs, define the test patterns and brightness control behavior explicitly. A small bright region and a largely bright screen can produce different power and thermal conditions. Compare suppliers under conditions that reflect the intended interface, including persistent elements and representative full-screen content where appropriate.
Appearance criteria need similar discipline. Terms such as “no visible mura” leave room for disagreement unless the protocol specifies observation conditions and acceptance boundaries. Define relevant defect categories, inspection lighting, viewing distance, image patterns, and the treatment of defects in critical screen areas. Photographs can support an inspection record, but camera processing and exposure make them insufficient as the sole basis for judging subtle uniformity differences.
Reliability must connect stress exposure to usable performance
A shared reliability plan should cover the failure mechanisms relevant to the product: luminance loss, color drift, differential aging, moisture sensitivity, electrical instability, and mechanical damage. The chosen exposures should reflect the application and assembly, including storage, transport, and operating conditions where they matter.
Agree on measurements before and after exposure. A display that still turns on may nevertheless have unacceptable color variation or image retention. Acceptance therefore needs to describe retained performance, alongside functional survival.
Accelerated aging results require careful interpretation. Different OLED constructions and operating conditions may respond differently to stress. A supplier’s extrapolated lifetime should include its endpoint definition, test conditions, and modeling assumptions. If those assumptions do not represent the buyer’s usage profile, the result may help screen candidates but cannot support an unqualified service-life promise.
Sample selection is equally important. Require a sampling plan that represents the production source being approved and addresses variation across relevant lots. Qualification samples prepared through exceptional controls offer weak evidence for routine supply. The protocol should explain how failures, retests, and deviations affect the approval decision.
Electrical compatibility belongs in the shared baseline
Matching dimensions and connector positions does not establish interchangeability. Check power sequencing, voltage requirements, initialization commands, timing, supported operating modes, sleep and wake behavior, and fault recovery. Differences can affect firmware, power consumption, thermal performance, or startup reliability.
Where the product uses touch sensing or bonded optics, verify interactions within the complete assembly. A panel may pass its own tests while the integrated display produces touch interference, optical artifacts, or mechanical stress. Supplier comparison should include enough system testing to reveal these effects before a second source enters production.
The resulting approval record should identify the panel and module revision, driver configuration, production site, test procedure revision, sample history, and any accepted deviations. This gives every supplier a common evidentiary standard without assuming their designs are identical.
Keep destination-market requirements and factory approval explicit
Supplier nationality is an unreliable shortcut for compliance. The relevant questions are where the finished product will be sold, how it is classified, what role the display plays, and which party carries the legal obligations. A common technical protocol can travel across borders; its regulatory attachments must follow the destination and product category.
For example, EU RoHS requirements may be relevant to an electrical or electronic product within scope, while REACH obligations depend on the applicable substance and article conditions. These frameworks address different obligations. A generic “environmentally compliant” declaration does not show which requirements were assessed, which materials were covered, or whether the declaration corresponds to the supplied revision.
Request evidence tied to the actual module and its constituent materials where necessary. A declaration or test report should identify its scope and allow the buyer to connect it to the purchased item. Changes to adhesives, coatings, flexible circuits, or other materials may require renewed review even when the display’s optical specifications remain unchanged.
Safety and electromagnetic compatibility also need the right assessment boundary. Component documentation can support the finished product’s evaluation, but it does not establish that every enclosure, power supply, cable arrangement, or installation meets the applicable requirements. Automotive displays may carry additional customer and application requirements. A quality management certificate can support confidence in process controls; it does not prove an individual OLED meets a particular reliability or safety requirement.
Separate regional obligations from factory approval in the qualification record. Each manufacturing site should demonstrate the relevant process controls, lot genealogy, inspection capability, handling practices, and change notification procedures. Shared ownership or an identical part number is insufficient evidence that another site produces equivalent output.
Cross-border evidence also needs clear interpretation. Use controlled terminology, consistent units, and agreed report formats. Where laboratory competence or accreditation is required, check that the relevant method falls within the stated scope. Resolve ambiguous translations before approval, especially where they affect acceptance limits or material declarations.
Use a staged process to approve and maintain shared criteria
A shared framework becomes useful when it reduces repeated work while preserving a clear decision trail. Organize the process around a common protocol, application validation, and destination-specific review. Each layer should have an owner and a defined approval outcome.
Build one controlled protocol and a supplier evidence matrix
Write the core requirements once, with test methods, acceptance limits, reporting rules, and change triggers. Then map each supplier’s evidence against them. Record whether a requirement is supported, requires additional testing, or has an approved deviation. This exposes gaps that a collection of supplier brochures would conceal.
Reuse evidence only when its scope matches the proposed supply. Existing results may be useful for the same construction, revision, manufacturing site, and test conditions. A related product family can provide context, but differences affecting optical, electrical, mechanical, or aging behavior need their own assessment.
Confirm disputed results and validate the assembled product
If suppliers report conflicting results, first compare methods and sample preparation. Repeating tests without resolving differences in drive conditions or measurement geometry can reproduce the disagreement. Where necessary, use a mutually accepted laboratory and controlled samples to establish a comparable result.
Next, test the candidate in the intended enclosure with the production firmware, power system, bonding arrangement, and representative screen content. This step connects component approval to product performance. It also identifies whether an alternative requires calibration, firmware changes, or mechanical adjustments before it can become a usable second source.
For connected terminals, concurrent software changes need attention. A team asking, “How do we move deployed AI-IoT devices to a new cloud provider?” may also change the dashboard or device behavior during that migration. If those changes increase screen-on time, persistent content, or brightness, review the display’s usage assumptions. Cloud migration remains a separate engineering task, but altered display duty can affect an existing OLED qualification.
Approve a defined configuration and control subsequent changes
Approval should name the configuration and conditions it covers. A supplier may be approved for one indoor terminal and remain unqualified for an outdoor control unit. Record operating restrictions, accepted deviations, and any supplier-specific integration requirements so purchasing decisions do not silently expand the approval scope.
Require notification of changes that could affect qualified performance, including relevant materials, processes, production sites, driver revisions, and module construction. Agree in advance which changes require document review, targeted testing, or full requalification. This prevents every minor adjustment from triggering the same response while retaining scrutiny of changes with material consequences.
Finally, connect incoming inspection and field returns to the approval record. Lot identification, defect classification, and failure analysis should make it possible to detect divergence from qualified production. A common protocol has continuing value only if the supplied product remains traceable to the configuration that passed it.
OLED suppliers in different countries can work to the same qualification criteria when the buyer defines equivalence precisely. The defensible sourcing decision is an approval tied to an application, a configuration, a production source, and a destination-market review. Another supplier can earn that approval through comparable evidence, giving procurement a usable alternative with known integration conditions.
Facing technical bottlenecks in manufacturing or looking for more efficient industrial solutions? Leave your details below and let the engineering experts at G-MDI solve them for you.
We respect your privacy. Your information is strictly confidential.
Recommended News
- Logic & Memory ICs (7nm/sub-7nm)Indian Minister Calls for Domestic Semiconductor Machinery and Precision ComponentsIndia’s semiconductor machinery and precision components push could reshape sourcing. Discover what the minister’s call means for suppliers and buyers.
- Logic & Memory ICs (7nm/sub-7nm)Automotive Technology Platforms in North America: What Do They Offer?Explore what an automotive technology platform in North America offers, from connected vehicles and EV charging to software, safety and deployment.
- Logic & Memory ICs (7nm/sub-7nm)GlobalFoundries Breaks Ground on $10 Billion New York Semiconductor FabGlobalFoundries breaks ground on a $10 billion New York semiconductor fab. Explore its planned 2029 production and potential supply chain impact.
- Industrial Smart WearablesIndustrial Smart Wearables: How to Evaluate Safety and ConnectivityIndustrial Technology Information Platform insights help you evaluate smart devices for workplace safety, connectivity and reliable response. Explore the guide.
- Logic & Memory ICs (7nm/sub-7nm)Samsung Starts Onyang HBM Packaging Plant, Moving Production Up to 2028Samsung's Onyang HBM packaging plant targets mass production in June 2028. Explore what the accelerated schedule could mean for suppliers and buyers.
- Logic & Memory ICs (7nm/sub-7nm)Choosing a Telecom Infrastructure Monitoring Platform: Key Evaluation CriteriaCompare telecommunications infrastructure platform monitoring solutions by coverage, interoperability, security, scalability, and real-world performance.